Open Nav
Moisture is one of the most underestimated sources of defects in surface mount technology assembly. Components that have absorbed atmospheric moisture before soldering can crack, delaminate, or develop internal voids when they are exposed to the rapid temperature ramp of reflow soldering. These failures, often grouped under the term popcorning, create field reliability problems that are difficult to detect during incoming inspection and expensive to address after the assembly is complete. Managing moisture sensitivity is not optional for manufacturers who want consistent, reliable production outcomes. It is a fundamental process control requirement that touches component storage, assembly planning, and quality verification.
The electronics industry addresses moisture sensitivity through a standardized classification system called Moisture Sensitivity Levels, or MSL. This system assigns each component a rating that indicates how much moisture it can absorb before it becomes at risk during reflow, and specifies the handling, storage, and floor life requirements that keep moisture-related defects to acceptable levels. Understanding MSL ratings, what they mean for your assembly process, and how to implement the controls they require is essential knowledge for anyone involved in SMT production, quality assurance, or procurement.
Modern surface mount components are made from materials that are inherently hygroscopic to varying degrees. Plastic IC packages, tape automated bonding substrates, and some passive components contain polymers and ceramics that absorb moisture from the air over time. This absorbed moisture is generally harmless as long as the component stays below a certain temperature threshold, but when the component is heated rapidly during reflow soldering, the moisture turns to steam and expands dramatically. If the pressure buildup is sufficient, it can crack the component package, delaminate internal layers, or create internal voids that compromise electrical connections.
The MSL classification system was developed by the Joint Electron Device Engineering Council, now part of JEDEC, to provide a consistent language for describing the moisture sensitivity of electronic components. Rather than leaving manufacturers to discover moisture sensitivity through trial and error, which would be prohibitively expensive and dangerous, the MSL system tells you upfront what a component can tolerate and what you must do to use it safely. The system covers component classification, labeling requirements, handling procedures, and floor life limits, giving manufacturers a complete framework for managing moisture risk.
Without MSL classification, the consequences of moisture damage would be far more widespread and severe. Popcorning failures create field returns that damage customer relationships and brand reputation, void warranties, and in safety-critical applications like automotive or medical electronics, can create liability exposure that far exceeds the cost of the component itself. The MSL system, properly implemented, reduces these failures to rare events caused by process breakdowns rather than systemic design flaws.
MSL ratings range from MSL 1 to MSL 6, with a higher MSL number indicating greater moisture sensitivity. Understanding what each level means in practical terms helps you make informed decisions about component handling and assembly scheduling.
MSL 1 components are rated for unlimited floor life at standard conditions of 30 degrees Celsius and 85 percent relative humidity. These components absorb moisture so slowly or tolerate it so well that they present essentially no moisture sensitivity risk under normal assembly conditions. They still need to be stored properly and protected from extreme conditions, but they do not require dry storage or careful floor life tracking. In practice, very few surface mount components qualify for MSL 1, and those that do are typically ceramic or metal packages rather than plastic.
MSL 2 components are rated for a floor life of one year at standard conditions before soldering. This level covers components that are mildly hygroscopic but tolerant of reasonable moisture exposure. Many passive components, connectors, and some less sensitive IC packages fall into this category. While MSL 2 components do not require dry storage, they should still be monitored for extended exposure to high humidity conditions that might exceed their one-year rating.
MSL 3 through MSL 5 cover increasingly sensitive components with shorter floor life limits. MSL 3 is rated for 168 hours of floor life at standard conditions, MSL 4 for 72 hours, and MSL 5 for 48 hours. Most plastic IC packages in common use fall somewhere in this range, with microcontrollers, memory devices, and processors frequently rated MSL 3 or MSL 4. Components in these categories must be tracked carefully from the time their dry storage packaging is opened, and assembly must be completed within the specified floor life window.
MSL 5a and MSL 6 represent the most sensitive components, with floor life of 24 hours for MSL 5a and mandatory bake before use for MSL 6. Components rated MSL 5a or higher are increasingly common in modern electronics as manufacturers push toward thinner packages and higher pin counts. These components demand the most rigorous handling controls and assembly planning to prevent moisture damage.
Behind the MSL floor life limits is a specific moisture absorption level that defines the boundary between safe and unsafe moisture content. Understanding this threshold helps explain why floor life limits are what they are and what happens when components exceed those limits.
JEDEC standards define the maximum moisture content for each MSL level based on the sensitivity of the component construction. A component reaches its critical moisture content when it has absorbed enough moisture that rapid heating to reflow temperatures would generate steam pressure sufficient to cause damage. The floor life limit for each MSL level represents the time it takes a component stored at standard conditions to reach this critical moisture content.
When a component exceeds its floor life, it has absorbed moisture beyond the safe threshold. This does not guarantee that damage will occur during reflow, because the actual risk depends on the specific reflow profile used, the thermal mass of the component, and manufacturing variations. However, components that have exceeded their floor life should be treated as at elevated risk, and whether to proceed with assembly or to dry bake them before use requires careful evaluation based on your quality requirements and risk tolerance.
Dry baking drives out accumulated moisture and resets the floor life clock, returning the component to its original safe condition. This process is specified by the component manufacturer and typically involves baking at 125 degrees Celsius for 24 to 48 hours, though some moisture-sensitive components require lower baking temperatures to prevent damage to the package or marking. Following the manufacturer's specified bake procedure is essential because incorrect baking can create other problems, including package cracking from thermal shock if the bake is followed by too rapid cooling.
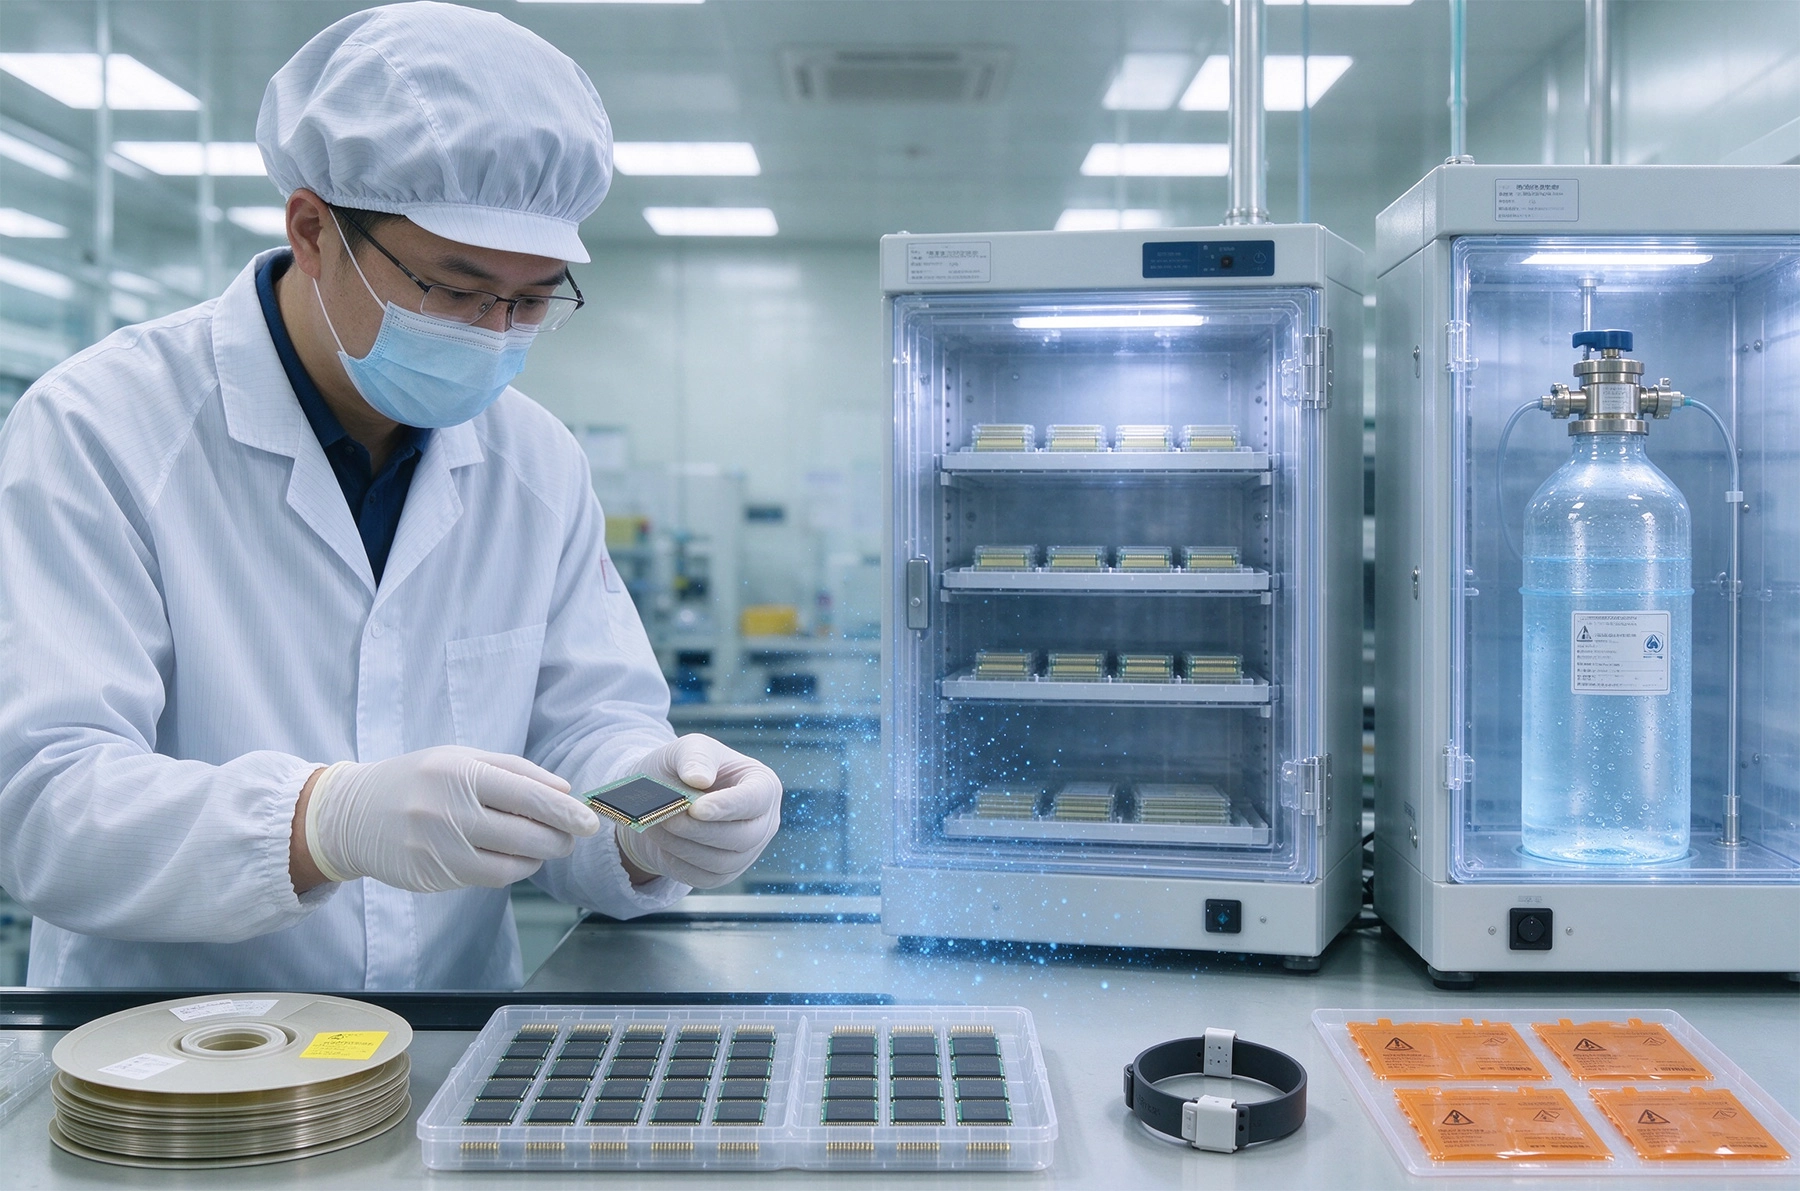
Preventing moisture absorption is far more cost-effective than dealing with the consequences of moisture damage. Dry storage keeps components below their critical moisture content indefinitely, eliminating the urgency of floor life tracking and reducing the risk of assembly defects. Implementing proper dry storage is the single most impactful improvement most SMT assemblers can make to their moisture sensitivity management.
Dry cabinets provide the most convenient dry storage solution for components that are in active use. These cabinets maintain an internal relative humidity typically below 5 percent through desiccant regeneration or purge drying, and they allow components to be stored in their original moisture barrier bags while still being accessible for production use. When a component is needed for assembly, it can be removed from the dry cabinet, used within its floor life, and returned to the dry cabinet if not fully consumed. This approach eliminates the need to track floor life for components in dry storage.
Dry storage bags with desiccant and humidity indicator cards provide a lower-cost alternative for components that are not in immediate use. Components received in moisture barrier bags should remain sealed until they are needed for assembly. The humidity indicator card inside the bag shows whether moisture has penetrated the barrier, allowing you to verify that the component arrived in good condition and has not absorbed significant moisture during storage. If the indicator shows moisture exposure beyond acceptable levels, the component should be dry baked before use.
The shelf life of sealed dry storage bags is typically specified by the component manufacturer and printed on the package label. This shelf life represents how long the moisture barrier remains effective under standard storage conditions. When the shelf life expires, the component must either be baked and resealed in fresh dry storage bags, or used within a shortened floor life window if the component's MSL rating allows for it. Treating sealed bags as permanently dry without regard for shelf life expiration is a common mistake that can lead to moisture damage despite proper initial storage.
Even with dry storage, components will eventually be removed from protection and exposed to the assembly environment. Managing floor life for these components requires clear procedures, accurate record keeping, and disciplined execution to ensure components are assembled within their safe exposure windows.
Floor life tracking begins the moment a component is removed from dry storage. The time of removal should be recorded, typically on a tracking label attached to the tray, reel, or tube of components. Assembly must be completed within the MSL-specified floor life from this point, and any components not used within that window must be returned to dry storage or dry baked before subsequent use.
Assembly line planning should account for the floor life constraints of the most sensitive components on the board. If your board contains an MSL 4 component with a 72-hour floor life, your production schedule must ensure that component is removed from dry storage no earlier than the assembly start time minus 72 hours. For large assemblies with long production cycle times, this constraint can dominate the production schedule if multiple sensitive components are present.
Partial reel or tray usage creates tracking complexity that is often underestimated. When a component reel is opened to remove some components for one assembly, the remaining components on the reel have already begun their floor life clock. Returning the reel to dry storage between uses pauses the floor life clock only if the reel is properly resealed in a dry storage bag with fresh desiccant. Simply placing the reel back on a shelf in the production area leaves the components exposed to ambient humidity and running their floor life clock continuously.
The reflow profile used for assembly directly affects the risk of moisture damage in sensitive components. Components at their moisture absorption limit may survive a conservative reflow profile while failing a more aggressive one, even if both profiles meet industry standards for other aspects of solder joint quality.
Ramp rate, the speed at which the assembly heats from room temperature to the peak reflow temperature, is the primary factor in moisture damage risk. Faster ramp rates give moisture less time to escape as steam before the solder melts, increasing pressure buildup inside the component package. A ramp rate of 1 to 3 degrees Celsius per second is generally recommended for moisture-sensitive components, while ramp rates above 3 degrees Celsius per second increase the risk of moisture-related failures.
Soak time, the period the assembly spends in the 150 to 200 degree Celsius range before reaching peak temperature, serves a dual purpose. It allows the assembly to reach thermal equilibrium so that all components are at similar temperatures, and it gives residual moisture in components time to escape before the peak temperature is reached. Profiles with no soak zone or very short soak times increase moisture damage risk for sensitive components.
Peak temperature should be the minimum necessary to achieve good solder joint formation, typically 5 to 10 degrees above the solder melting point. Higher peak temperatures increase stress on moisture-sensitive components and should be avoided when possible. For lead-free solders with higher melting points than tin-lead, the peak temperature requirement is inherently more challenging for moisture-sensitive components, which is one reason why moisture management has become more important as lead-free assembly has become universal.
Despite best efforts at prevention, moisture damage sometimes occurs. Recognizing the signs of moisture damage and understanding how to respond appropriately limits the impact of these events and prevents defective assemblies from reaching customers.
External signs of moisture damage include package bulging or swelling, cracks in the package body visible under magnification, and lifting of component pads from the board surface. These signs are relatively rare because most moisture damage occurs internally, but when they are observed, the affected assembly should be removed from production immediately and the component should be rejected.
Internal moisture damage is far more common and far more difficult to detect. Delamination between internal layers of the component package, cracks in the die attach material, and voids in the wire bond interface can all result from moisture-induced pressure during reflow. These defects are invisible from the external inspection and may not cause immediate failure, but they significantly reduce the component's long-term reliability, creating field failures that appear months or years after assembly. X-ray inspection and acoustic microscopy are the primary tools for detecting internal moisture damage.
When moisture damage is discovered, the response depends on the severity and the application. Single instances of damage on non-critical components may be handled through normal rework processes. Recurring moisture damage across multiple boards from the same component lot indicates a systemic problem with that lot or with the storage and handling procedures, and warrants investigation and corrective action before production continues.
Managing moisture sensitivity effectively requires accurate MSL information from your component suppliers. Without reliable data on the MSL rating of each component, you cannot implement appropriate storage and handling controls.
MSL ratings should be specified as a requirement when qualifying new components. Ask your component supplier for the JEDEC MSL rating for each part number you plan to use, and verify this information against the component datasheet or JEDEC registration. Some components have different MSL ratings depending on the specific package variant, so be sure to confirm the rating for the exact part you are purchasing.
Component datasheets and JEDEC registration documents provide the authoritative MSL rating and any associated handling requirements. These documents also specify any alternative MSL ratings that may apply if different reflow profiles are used, and they provide the dry bake requirements for components that have exceeded their floor life. Reviewing this documentation should be part of your component qualification process, not an afterthought that surfaces only when problems occur.
Traceability records linking component lot numbers to MSL classification and handling history support root cause investigation when moisture-related defects are discovered. If a batch of assemblies fails due to moisture damage, traceability records allow you to identify which component lot was involved, when it was received, how it was stored, and how long it was on the production floor. This information is essential for determining whether the failure was caused by a component defect or a process breakdown on your production line.
Effective moisture sensitivity management requires more than just knowing your components' MSL ratings. It requires systematic procedures, appropriate equipment, training for everyone who handles moisture-sensitive components, and audit trails that verify procedures are being followed consistently.
Begin with an inventory of the MSL ratings for all components you use in production. This inventory, often called an MSL matrix, allows you to quickly identify the most sensitive components on any given board and plan storage and handling requirements accordingly. Update this matrix whenever you qualify new components or when a component supplier changes the MSL rating for an existing part.
Invest in dry storage infrastructure appropriate to your production volume and component sensitivity mix. Even small production operations can benefit from at least one dry cabinet or a systematic approach to dry storage bag management. As production volume grows, the investment in additional dry storage capacity pays back through reduced defect rates and lower rework costs.
Train all personnel who handle moisture-sensitive components on the procedures and rationale for moisture management. Floor operators need to understand how to track floor life, when to return components to dry storage, and how to recognize potential moisture damage. Quality inspectors need to understand what to look for during inspection and how to respond when they suspect moisture-related defects. Engineering and management need to understand the business impact of moisture sensitivity so they prioritize the resources needed to manage it effectively.
Conduct regular audits of your moisture sensitivity management practices to verify that procedures are being followed and that they remain appropriate for your component mix and production environment. Audit findings should drive continuous improvement in your processes and training programs.
Moisture sensitivity is a manageable risk, not an unavoidable source of defects. By understanding MSL ratings, implementing appropriate dry storage, tracking floor life rigorously, and controlling reflow profiles for sensitive components, manufacturers can keep moisture-related defects to levels that support high-quality, reliable production. The investment in moisture management infrastructure and procedures pays back through lower rework rates, fewer field failures, and reduced liability exposure.
The most successful moisture sensitivity programs are built on systematic procedures, appropriate equipment, and a culture that takes moisture management seriously at every level of the organization. When everyone involved in component handling understands why moisture sensitivity matters and how to manage it, the procedures become habits rather than burdens, and the risk of moisture-related failures drops accordingly.
As electronic products continue to push toward smaller packages, higher pin counts, and thinner profiles, the moisture sensitivity challenge will only increase. Building strong moisture sensitivity management practices now prepares your organization for the increasingly demanding component landscape ahead.
Contact us to discuss your requirements and explore how moisture sensitivity management can support your SMT assembly quality goals.
Avoiding Tombstoning and Bridging in Your PCB LayoutJuly/30/2026
Panelization Strategies: Saving Money on Your PCB Assembly OrderOctober/27/2026
The Importance of NPI (New Product Introduction) in AssemblyNovember/02/2026
Inventory Management Benefits of Using a Turnkey Assembly PartnerAugust/03/2026
The Pros and Cons of Lead-Free vs. Leaded Solder in AssemblyOctober/26/2026